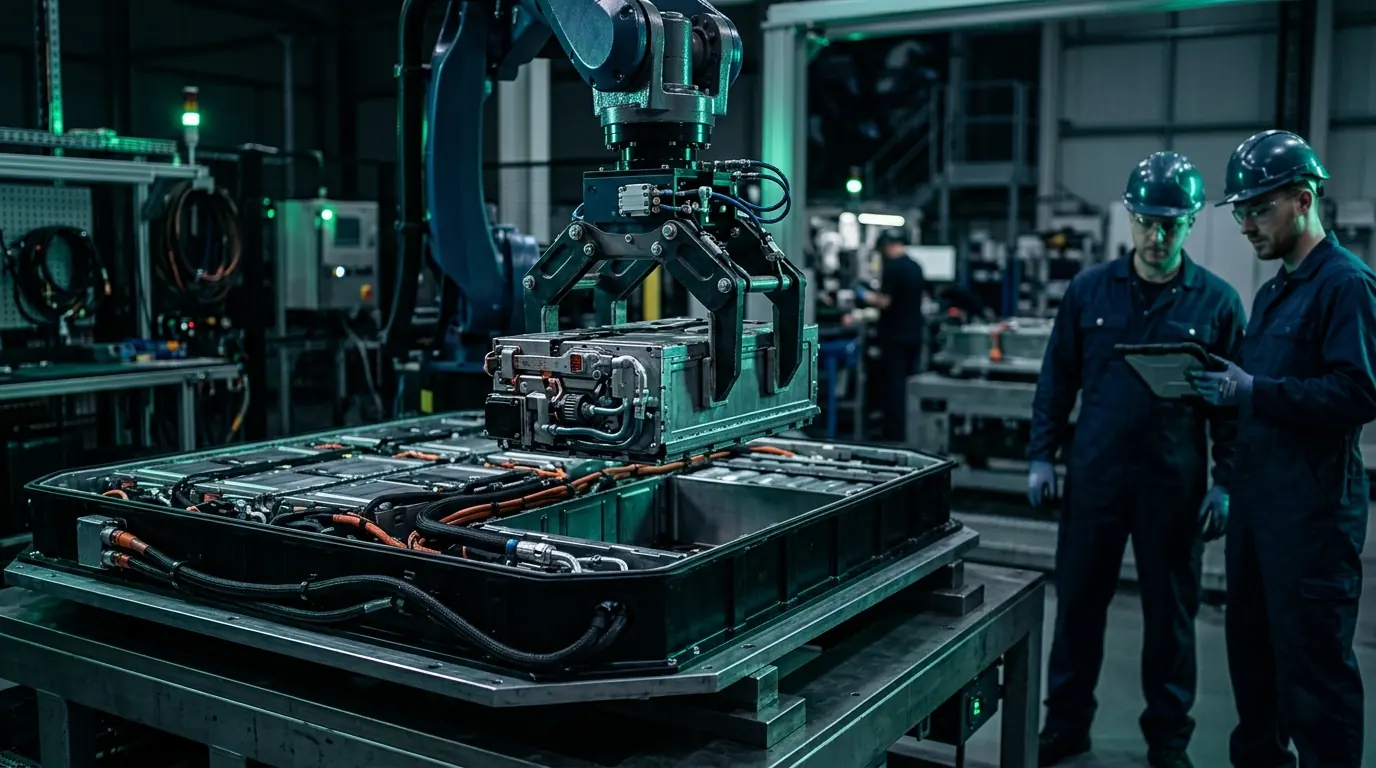
What the site does
Hosur, just across the Tamil Nadu border from Bengaluru, is one of India's largest two-wheeler manufacturing centres and has become a focal point for electric two-wheeler production. The diagnostics centre opened in SIPCOT Industrial Complex Phase III in 2021 to grade the small-format packs this belt produces in very large numbers, as well as retirements from Bengaluru's delivery and ride-hailing fleets.
Its 14,000 TPA of bench capacity is laid out for two-wheeler and three-wheeler packs and modules, alongside a smaller share of passenger-car packs. Because units are small and numerous, the centre measures throughput in thousands of units a week. Battery-swap operators are a growing source of intake, bringing packs with detailed usage histories that make grading faster and more accurate.
What arrives at the gate
Feedstock at Hosur, Tamil Nadu reflects its catchment and plant type. Every consignment is weighed, photographed and logged against the originating manifest before it enters the process area.
- Electric two-wheeler packs from the Hosur and Bengaluru belt
- Swappable battery units from urban swap networks
- Warranty and field returns from two-wheeler makers
- Passenger-car and delivery fleet packs from Bengaluru
The process, step by step
The 3 operating lines — module soh bench, eis diagnostics laboratory, ai optical cell grading — run the sequence below.
| Stage | What happens |
|---|---|
| Intake & safety triage | Packs are logged, thermally imaged and screened for swelling, coolant ingress or venting before entering the bench area. |
| Controlled de-energising | Residual energy is discharged to a safe state of charge with regenerative load banks and recorded per serial number. |
| Module-level capacity test | Full charge-discharge cycling at C/3 establishes usable capacity, internal resistance and cell-to-cell balance. |
| EIS fingerprinting | 1 mHz–10 kHz impedance sweeps separate SEI growth, lithium plating and contact resistance degradation modes. |
| AI optical inspection | Machine-vision inspection of busbars, welds and cell cans flags mechanical defects that block second-life reuse. |
| Grade assignment | Grade A (≥85% SOH), B (75–85%), C (65–75%) and D routes are assigned, with D-grade material released to refining. |
What sets the site apart
Small-format bench layout. Fixtures and cyclers sized for 2–5 kWh packs allow hundreds of units to be tested in parallel each day.
Swap-network data intake. Serial-level usage histories from swap operators are loaded before testing, cutting grading time and improving routing decisions.
Repair-or-retire diagnostics. Impedance fingerprinting separates packs worth repairing at cell or BMS level from those that should be retired.
Where material goes next
Material that Hosur, Tamil Nadu does not finish on site moves to the nearest specialist facility in the network, keeping transport distances and dwell times down.
| Facility | Role | Distance |
|---|---|---|
| Nagpur — Butibori Second-Life Works | Second-Life BESS Works | 918 km |
| Chennai — Sriperumbudur Recovery Campus | Hydrometallurgical Refinery | 230 km |
Field note